2026 Top Fusion Pipe Welder Buying Guide for Global Buyers
Global pipe infrastructure is expanding, yet welding quality remains uneven across regions. Energy, water, and industrial projects increasingly require reliable thermoplastic and polyethylene joining systems. For global buyers, choosing a Fusion Pipe Welder involves more than comparing heating plates and listed power ratings.
The American Welding Society’s Welding Workforce Data report projects a shortage of approximately 330,000 welding professionals in the United States by 2026. This pressure makes repeatable equipment, clear controls, and simple operator training increasingly valuable. According to MarketsandMarkets’ Welding Equipment Market research, automation and process consistency are major market trends. However, broad market forecasts cannot replace jobsite testing. A machine that performs well in a factory may struggle beside a dusty trench, under unstable voltage, or during cold-weather installation.
Standards matter. ISO 21307 defines butt-fusion procedures for polyethylene piping, while ASTM F2620 provides recognized guidance for polyethylene pipe joining. Buyers should check whether equipment supports the required pipe diameter range, pressure records, heating temperature, and data traceability. Small details matter.
This guide compares those practical factors for international purchasing teams. It examines machine structure, hydraulic performance, controller accuracy, transport design, service support, and total ownership cost. It also considers regional voltage, spare-part availability, operator training, and documentation quality. Reports provide direction, not certainty. A spreadsheet can still mislead. Real experience often exposes hidden costs, especially when replacement heaters or hydraulic seals arrive late. Wise buyers should verify specifications, request test welds, and question unusually low prices before approving a purchase.
What Is a Fusion Pipe Welder and How Does It Work?
What Is a Fusion Pipe Welder and How Does It Work?
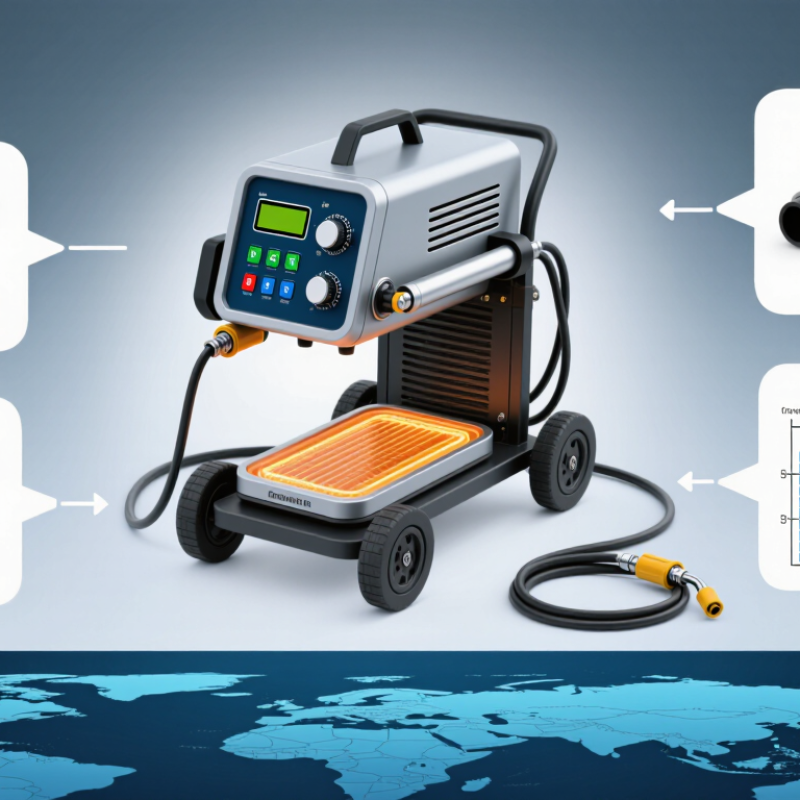
A fusion pipe welder joins thermoplastic pipes by softening their mating surfaces with controlled heat. It is commonly used with polyethylene and polypropylene piping systems. Unlike threaded connections, fusion creates one continuous plastic joint. The equipment usually includes a heating plate, clamps, alignment guides, hydraulic controls, and temperature monitoring. A stable frame matters because even slight pipe movement can weaken the finished connection.
During butt fusion, an operator clamps two pipe ends and checks their alignment. A facing tool removes uneven material from both surfaces. The heated plate then contacts the pipe ends until a consistent melt bead appears. The plate is removed, and the softened ends are pressed together under controlled pressure. They remain fixed during cooling. The joint should show a balanced bead around the pipe, without contamination, gaps, or excessive distortion.
The process looks simple. It is not forgiving. Dust, moisture, incorrect pressure, or poor alignment can affect performance. Field inspectors often examine bead shape, heating time, cooling time, and machine records. Socket fusion uses heated fittings instead, while electrofusion uses embedded wires to melt fitting surfaces. Each method requires different tools and procedures. A larger machine is not automatically better. Buyers should match pipe diameter, material, jobsite power, temperature control, and operator training. In real work, rushed cooling is a common mistake. A joint may look acceptable and still deserve closer inspection.
| Welder Type | What It Is | How It Works | Typical Pipe Size Range | Common Materials | Typical Heating or Electrical Parameters | Typical Power Requirement | Automation and Control | Main Advantages | Key Buying Considerations |
|---|---|---|---|---|---|---|---|---|---|
| Manual Butt Fusion Welder | A compact machine that joins two thermoplastic pipe ends directly. | The pipe ends are faced, heated against a hot plate, brought together under controlled pressure, and held until the joint cools. | Approximately 20–160 mm outside diameter, depending on the frame and inserts. | PEPP | Hot-plate temperature is commonly about 200–230°C for polyethylene applications; the approved pipe procedure determines the actual setting. | Approximately 1.5–3.0 kW for many small and medium machines. | Manual temperature reading, clamping, alignment, pressure, and timing. | Portable, relatively low purchase cost, and suitable for repair work or small projects. | Check alignment accuracy, clamp rigidity, insert availability, temperature stability, and operator access in the work area. |
| Hydraulic Butt Fusion Welder | A powered butt-fusion system designed for larger diameters and higher joining forces. | Hydraulic cylinders move the clamped pipes through facing, heating, changeover, fusion, and cooling stages. | Approximately 63–1,600 mm outside diameter, depending on machine configuration. | PEPP | For polyethylene, hot-plate operation is commonly within about 200–230°C; fusion force and cooling time are calculated from the approved procedure. | Approximately 3–15 kW, with larger machines requiring more hydraulic and heating capacity. | Hydraulic pressure control; advanced models may provide automatic cycles, data recording, and barcode-based job traceability. | Consistent joining force, improved productivity, and suitability for water, gas, drainage, and industrial pipelines. | Compare maximum diameter, hydraulic pressure range, carriage travel, data logging, generator compatibility, and transport requirements. |
| Socket Fusion Welder | A small heating tool used to join pipe ends to matching sockets, fittings, or valves. | The outside of the pipe and inside of the fitting are heated simultaneously with matched heating bushes, then pressed together and allowed to cool. | Approximately 16–110 mm outside diameter for common handheld and bench-mounted equipment. | PP-RPPPE | Heating tools commonly operate around 250–270°C, but the correct temperature, heating time, insertion depth, and cooling time depend on material and wall thickness. | Approximately 0.8–2.5 kW. | Usually manual; electronic temperature regulation and interchangeable heating bushes are common. | Fast setup, low weight, and practical for building services, plumbing, irrigation, and confined spaces. | Check bush coating quality, temperature recovery, calibration method, socket-size range, and availability of replacement heating sets. |
| Electrofusion Control Unit | An electronic power and control unit used with electrofusion fittings that contain embedded resistance wires. | The unit supplies a controlled electrical current to the fitting. The resistance wires melt the interface between the fitting and pipe, forming a fused joint during cooling. | Commonly approximately 20–710 mm outside diameter; larger systems are available for specific applications. | PEPE100 | Voltage, current, fusion time, and compensation are determined by the fitting manufacturer or barcode procedure; the operator should not select values by guesswork. | Approximately 1.5–5 kVA for many portable units, depending on fitting size and duty cycle. | Microprocessor control, barcode scanning, automatic fusion-cycle monitoring, error detection, and joint data storage may be available. | Useful in restricted spaces, for repairs, and for tapping or joining fittings where butt fusion is impractical. | Check output range, barcode compatibility, generator performance, cable length, data export, protection rating, and calibration service. |
| Automatic CNC or Data-Logging Fusion Machine | An advanced butt-fusion platform that automates the joining sequence and records process data. | The machine controls facing, heating, pressure changes, fusion force, timing, and cooling according to stored pipe parameters or an approved welding procedure. | Approximately 63–1,600 mm outside diameter, depending on the equipment class. | PEPP | Temperature, pressure, time, pipe diameter, wall thickness, and ambient conditions may be monitored and recorded throughout the cycle. | Approximately 4–20 kW, depending on diameter, hydraulic system, and heating plate size. | High automation, digital displays, operator prompts, alarms, electronic reports, and USB or network data transfer on some models. | Improves repeatability, documentation, training control, and project quality assurance. | Evaluate software language support, report format, calibration records, password permissions, data security, and after-sales technical support. |
| Portable Battery-Assisted Fusion System | A compact fusion solution designed for field work where mains electricity or large generators are unavailable. | A battery pack powers the heating element, control electronics, or hydraulic functions, while the joint follows the selected butt-fusion or electrofusion procedure. | Often approximately 20–160 mm for portable applications, subject to battery capacity and machine design. | PEPP | Operating temperature and fusion parameters remain procedure-dependent; battery voltage and capacity determine the number of joints per charge. | Battery systems are commonly specified by voltage and capacity rather than continuous mains power; actual output varies by model. | Digital battery monitoring, temperature control, cycle timing, and job records may be included. | Low emissions at the work point, easier transport, and greater flexibility for emergency or remote repairs. | Check battery runtime, recharge time, spare-battery cost, low-temperature performance, transport regulations, and replacement availability. |
| Pipeline Workshop Fusion Machine | A heavy-duty stationary or trailer-mounted system intended for repetitive prefabrication and high production volume. | Pipe sections are clamped and fused in a controlled workshop environment before being transported or installed on site. | Approximately 315–2,000 mm or more, depending on the machine design. | PEPP | Usually includes controlled heating-plate temperature, hydraulic fusion force, programmed changeover, and extended cooling control. | Approximately 8–30 kW or higher for very large pipe systems. | Hydraulic or fully automatic control, production records, operator login, and repeatable welding recipes may be provided. | High throughput, stable alignment, reduced manual handling, and improved process consistency. | Assess floor space, lifting equipment, transport method, electrical supply, pipe support system, and total lifecycle cost. |
| Buyer’s technical note: Actual pipe-size capacity, power demand, heating temperature, fusion pressure, heating time, changeover time, and cooling time vary by machine, pipe material, outside diameter, wall thickness, ambient temperature, and approved joining procedure. Common reference documents include ISO 21307, ASTM F2620, ISO 12176-1, ISO 12176-2, and applicable national pipeline standards. Always verify the machine settings against the pipe and fitting manufacturer’s qualified procedure. | |||||||||