top of page

Why Choose a Fusion Welding Machine for Global Projects?

Why Choose a Fusion Welding Machine for Global Projects?

Global infrastructure projects demand joints that remain dependable under pressure, temperature changes, and difficult site conditions. A Fusion Welding Machine supports this goal by joining thermoplastic pipes through controlled heating, alignment, and pressure. Unlike mechanical couplings, a properly fused joint can create a continuous connection with fewer leak paths. That matters beside highways, under cities, and across remote construction zones.

Dr. John J. Grewell, a recognized plastics-joining specialist, emphasizes, “Welding is a process, not a product.” His point is practical. Machine quality alone cannot guarantee a reliable joint. Operators need correct temperature settings, clean pipe ends, stable clamping, and documented cooling time. A technician may notice a thin bead, uneven pressure, or slight misalignment before the joint leaves the site. These details can determine long-term performance.

Global teams also benefit from repeatable procedures and digital records. A modern Fusion Welding Machine can help control heating cycles, pressure levels, and alignment more consistently. It can support training across different crews and reduce avoidable variation. However, this advantage is not automatic. Poor maintenance, rushed preparation, or unsuitable site conditions can still weaken results. That limitation deserves attention.

Project engineers should evaluate pipe materials, diameter ranges, power requirements, portability, and local service support. They should also review applicable standards and require qualified operators. A machine may perform well in a factory but struggle in wind, rain, dust, or unstable ground. Choosing the right equipment means examining the entire welding process, not only the machine’s specification sheet.
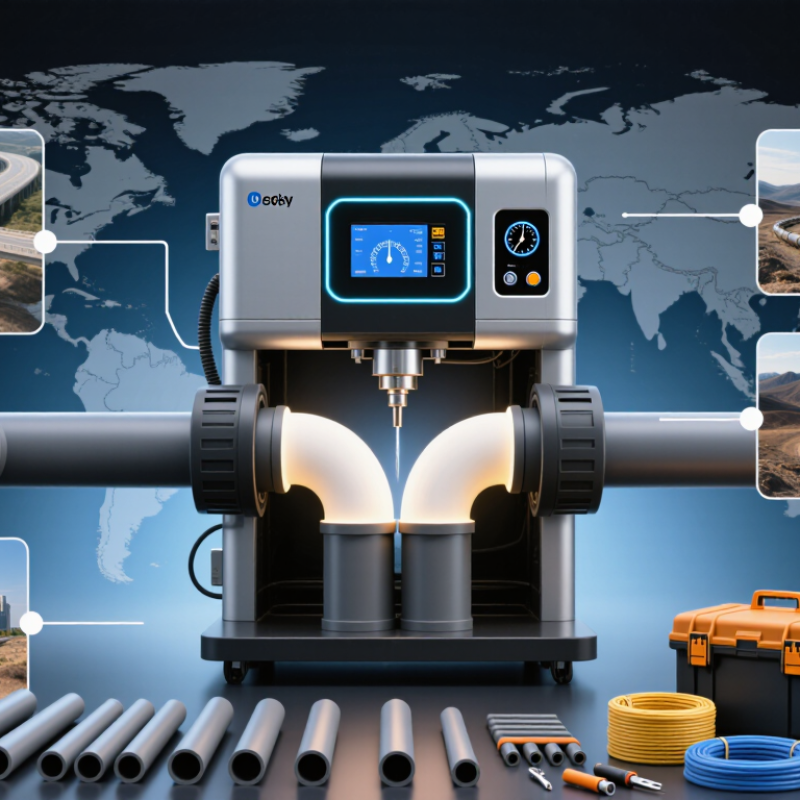
Why Choose a Fusion Welding Machine for Global Projects?

What Is a Fusion Welding Machine?

A fusion welding machine joins thermoplastic pipes by heating their prepared surfaces and applying controlled pressure. The softened materials cool into one continuous joint. It is not a glue gun. No separate adhesive is required.

A typical butt-fusion system includes clamps, a facing tool, heater plate, hydraulic unit, and control panel. The machine aligns pipe ends, removes uneven surfaces, heats them, and records joining pressure and time. Field technicians usually check clean faces, correct temperature, bead formation, and cooling stability. These details matter on long water, gas, and industrial utility lines. Standards such as ISO 21307 and ASTM F2620 define recognized procedures for polyethylene pipe fusion.

Infrastructure demand makes this equipment increasingly relevant. The U.S. Environmental Protection Agency’s 7th Drinking Water Infrastructure Needs Survey estimates $625 billion in drinking-water investment needs from 2023 to 2042. The agency’s Clean Watersheds Needs Survey reports another $630.1 billion for wastewater infrastructure through 2041. These figures do not measure fusion machines directly. They show the scale of pipe-related work ahead. A reliable machine can improve repeatability, reduce alignment errors, and create traceable records across projects. Still, equipment alone cannot guarantee joint quality. Poor preparation, untrained operators, or rushed cooling can weaken an otherwise sound connection. That uncomfortable point deserves more attention.

How Fusion Welding Machines Work

Why Choose a Fusion Welding Machine for Global Projects?

How Fusion Welding Machines Work

A fusion welding machine joins thermoplastic pipes by heating their surfaces until they soften. The machine then presses both ends together and holds them during cooling. No adhesive is needed. The joint becomes one continuous polymer structure.

In butt fusion, clamps keep the pipes aligned. A facing tool removes oxidation and uneven edges. A heated plate warms the pipe ends, commonly between 204°C and 232°C, according to the Plastics Pipe Institute’s Handbook of Polyethylene Pipe. The plate is removed quickly. Pressure follows. ASTM F2620 requires controlled heating, joining, and cooling steps. Small errors matter. Poor alignment can weaken the entire connection.

Electrofusion works differently. Fittings contain embedded resistance wires. An electrical current heats the fitting and pipe surfaces together. ISO 21307 describes three recognized butt-fusion procedures, showing why pressure and timing must match the pipe material. Field teams should record ambient temperature, heating time, joining pressure, and cooling time. Digital traceability helps during inspections, but it cannot replace skilled observation. The process is reliable, not foolproof.

Tips: Clean and dry every surface before heating. Check calibration before mobilization. Protect hot plates from dust and wind. Allow full cooling before removing clamps. A simple checklist prevents expensive rework.

Why Choose a Fusion Welding Machine for Global Projects? - How Fusion Welding Machines Work

Typical characteristics for thermoplastic pipe fusion equipment. Actual settings must follow the applicable project specification, material data, and welding standard.
Data Dimension How It Works Typical Technical Data Global Project Value
Primary joining principle Matching thermoplastic surfaces are heated until softened, brought together under controlled force, and allowed to cool into one continuous joint. A solid-state joint is formed without metal filler, adhesives, or threaded fittings. Supports leak-resistant pipeline construction and reduces the number of separate connection components.
Main process: butt fusion Pipe ends are clamped, faced square, aligned, heated against a plate, joined, and held under pressure during cooling. Commonly used for compatible polyethylene and polypropylene pipe systems; joint parameters depend on pipe size, wall thickness, resin, and standard. Suitable for water, gas, mining, industrial, and utility projects when the pipe system is approved for fusion joining.
Main process: electrofusion An electrically heated wire embedded in a fitting melts the fitting and pipe interface; cooling completes the joint. Requires compatible electrofusion fittings, a controlled power supply, clean surfaces, correct scraping, and barcode or manual parameter input where specified. Useful in confined areas, repair work, tie-ins, and locations where butt-fusion equipment cannot be positioned easily.
Compatible materials Heat and pressure are selected according to the specific thermoplastic resin and approved joining procedure. Common materials include PE80, PE100, PE4710, and PP grades; dissimilar materials should not be fused unless the governing procedure explicitly permits it. Material-specific controls make the equipment adaptable to regional pipe standards and different utility applications.
Heating temperature A coated heating plate transfers heat evenly to the prepared pipe ends before the surfaces are pressed together. Typical controlled plate settings are approximately 200–230 °C for polyethylene and about 210–240 °C for polypropylene, subject to the approved procedure. Digital temperature control helps maintain repeatable results across different climates and work crews.
Alignment and clamping Hydraulic or mechanical clamps hold the pipes, while the facing tool removes oxidation, dirt, and uneven end surfaces. The machine must accommodate the pipe outside-diameter range and provide sufficient restraint against movement and wind loads. Improves joint consistency and reduces dependence on manual alignment in large-diameter installations.
Fusion pressure and force The operator or control system applies the force required for bead formation, heating, changeover, joining, and cooling. Values are calculated from pipe geometry, material, machine hydraulic area, and the applicable standard; there is no universal pressure value. Programmable or monitored force reduces operator variation and supports documented quality assurance.
Cooling and joint handling The newly joined pipe ends remain clamped and undisturbed until the specified cooling time has elapsed. Cooling time increases with wall thickness and is defined by the approved procedure; forced cooling with water or compressed air is generally avoided unless specifically allowed. Protects joint integrity in hot, cold, windy, or remote installation environments.
Typical equipment range Machines use interchangeable inserts, clamps, and facing tools to cover different pipe diameters. Portable units commonly serve small and medium diameters; larger hydraulic machines are used for heavy-wall and large-diameter pipe. The exact range is model-specific. A modular equipment fleet can support water, gas, drainage, and industrial networks across multiple project sizes.
Power requirements Electric heating plates and facing tools are powered by a suitable electrical supply; hydraulic systems may use manual, electric, or engine-driven power packs. Voltage, frequency, current, and generator capacity must match the machine nameplate and local electrical requirements. Configurable power options help teams work at permanent facilities, temporary sites, and remote locations.
Quality control The machine controls or records temperature, pressure, time, pipe size, and operator actions throughout the fusion cycle. Visual bead inspection is commonly supplemented by procedure checks, dimensional verification, and selected non-destructive or destructive testing where required. Traceable records support audits, handover documentation, and consistent acceptance criteria across international teams.
Relevant standards The machine and procedure are selected to meet the pipe material, application, and jurisdictional requirements. Common references include ISO 21307, ASTM F2620, ISO 12176, and regional utility specifications; the project contract determines which standard governs. Standards-based procedures simplify engineering review and help harmonize practices across countries.
Key advantages Controlled heat, alignment, force, and cooling produce a joint from the pipe material itself. No solvent curing; no metal filler; low routine consumable demand; repeatable process when equipment and procedures are properly maintained. Offers a practical combination of durability, installation flexibility, quality traceability, and reduced fitting complexity for global infrastructure projects.

Key Benefits for International Construction Projects

Global construction needs reliable pipe joining in difficult places. Fusion welding machines offer a practical solution for thermoplastic pipelines. They heat and join pipe ends into one continuous connection. This reduces dependence on metal fittings and minimizes potential leak points. The Global Infrastructure Hub estimated a worldwide infrastructure investment gap of 15 trillion dollars by 2040. Durable installation methods therefore matter.

Fusion equipment also supports consistent work across borders. Modern machines can control heating temperature, pressure, and joining time. Operators can record these values for inspection and project documentation. ISO 21307 provides recognized guidance for polyethylene butt fusion procedures. This helps contractors align field practices across different teams and regions. It also makes training easier. Still, machines do not replace skilled technicians.

The water sector shows why reliability is urgent. The WHO and UNICEF Joint Monitoring Programme reported that 2.2 billion people lacked safely managed drinking water in 2022. International projects often face dust, rain, unstable power, and limited workshop space. A portable fusion machine can work closer to the installation area. Fewer transported fittings may simplify logistics. That sounds ideal, but reality is less tidy. Poor surface preparation, incorrect alignment, or rushed cooling can weaken a joint. Experienced crews should verify pipe condition, calibration, weather limits, and recorded parameters before approving each connection.

Factors to Consider When Choosing a Machine

Why Choose a Fusion Welding Machine for Global Projects?

Selecting a fusion welding machine requires more than checking heating temperature and pipe size. Project teams should examine material compatibility, welding range, pressure control, and operating accuracy. A machine used on remote sites must tolerate dust, rain, and unstable power. Transport weight also matters when equipment moves between roads, ports, and elevated work areas. I have found that simple controls reduce mistakes during rushed installation work. However, “simple” should not mean poorly documented.

Certification and traceability deserve careful attention. Confirm that the machine supports the required regional standards and project specifications. Ask for calibration records, inspection procedures, and clear operating instructions. Data logging can help verify temperature, pressure, heating time, and joint quality. Local service access is equally important. A small sensor failure can stop an entire crew. Training should include practice on actual pipe materials, not only classroom demonstrations. A perfect specification rarely exists. Teams must accept trade-offs, but they should record them honestly.

Tips: Compare total operating cost, not only the purchase price. Check spare parts availability before shipment. Test the machine with site power conditions. Leave room for operator feedback. It may reveal problems missed during factory trials.

Applications, Standards, and Project Compatibility

A fusion welding machine suits global projects when its process matches the pipe, site, and governing standard. Water transmission, wastewater, gas distribution, mining, and industrial lines commonly use thermoplastic pipes. The Global Infrastructure Hub estimated that the world needed about $94 trillion in infrastructure investment by 2040, with an $18 trillion gap. That scale demands repeatable joining, not improvised heating.

Standards define compatibility more clearly. ISO 21307 describes butt-fusion procedures, while ASTM F2620 addresses polyethylene pipe and fittings. ISO 12176 also covers equipment requirements and traceability. In practice, a machine should control heating temperature, pressure, alignment, and cooling time. Data logging helps inspectors verify each joint beside a muddy trench or inside a temporary workshop. It also supports quality records across different countries.

Power supply matters.

A 400-volt unit may fail on a remote site without suitable electrical infrastructure. Cold weather, dust, humidity, and uneven ground can also change operating conditions. Project teams should check pipe diameter ranges, SDR compatibility, generator capacity, calibration records, and operator training before shipment. A machine that performs well in a factory may struggle at high altitude. I have seen specifications treated as guarantees; they are not. Site trials and documented procedures remain necessary, especially when local codes add requirements beyond ISO or ASTM guidance. The machine is only one part of the weld.

Concrete Products Unlimited

Mon-Fri 8AM - 5PM

Concrete products, wholesale Arizona river rock for landscaping, decorative rock, sand and gravel. Rock quarry located in Arizona and delivers throughout the USA.

©2003 by Concrete Products Unlimited

bottom of page